 Английский язык
 Французский язык
 На испанском языке
 Русский язык
 Корейская народно-демократическая республика
 На японском языке
Low-Dust Black Rice Extract Minimizes Cross-Contamination in Solid Dosages
Airborne Dust Risks in High-Speed Solid Dosage Lines
High-speed tableting and capsule-filling lines face a critical manufacturing threat: : категория:severe airborne dust emission leaking from traditional botanical extract fine powders- да- да- да- да- да. Escaping particulate matter routinely bypasses feed hoppers and mechanical seals, contaminating pharmaceutical cleanrooms and breaching critical HVAC containment zones.
This uncontrolled particulate migration drives batch-to-batch cross-contamination, serving as a primary trigger for regulatory compliance failures under global safety standards. Furthermore, heavy ambient dust forces plant managers to execute extended decontamination teardowns, spiking labor costs and stalling profitable batch changeovers.
Established in 2000, Технология "зеленый источник" solves these high-throughput manufacturing bottlenecks through 26 years of specialized botanical extraction expertise. Our advanced solid dosage raw materials successfully eliminate raw material vulnerability on automated compression lines, allowing global dietary supplement brands to secure absolute batch uniformity, flawless regulatory compliance, and streamlined plant operational efficiency (OEE).
Advanced Particle Engineering: The Mechanics of "Low-Dust"
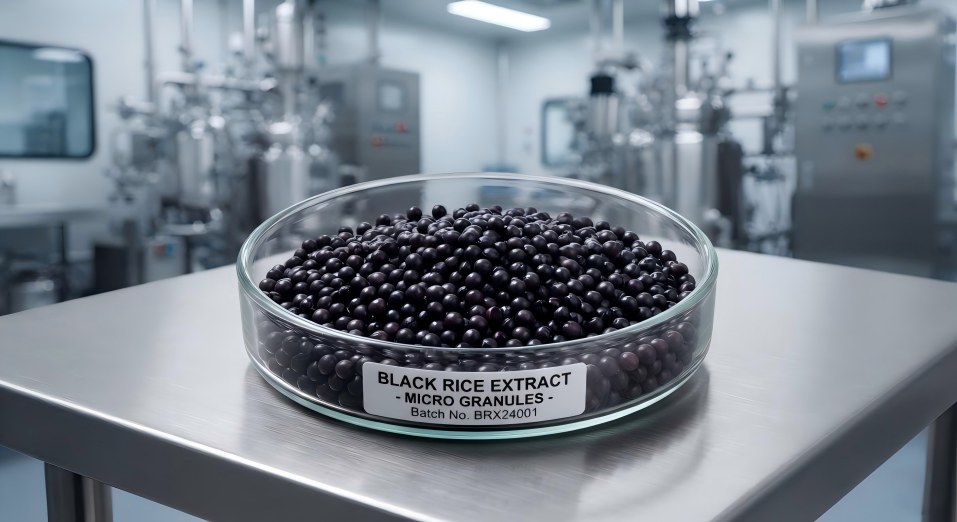
Traditional botanical extracts fail in high-throughput lines due to poor morphology, but Green Spring Technology resolves this via advanced fluid-bed granulation. This particle engineering process aggregates ultra-fine particles into uniform, free-flowing micro-granules without altering the molecular structure of the botanical matrix.
By shifting the particle size distribution away from dust-prone fine mesh, our engineered micro-granules deliver three core physical and chemical advantages:
Optimized Carr Index Metrics: Provides superior bulk density, optimized hopper flow, and zero mechanical bridging inside high-speed compression equipment.
Precision Thermal Dynamics: Guarantees zero degradation of fragile active pigments during the agglomeration process, securing 100% standardized Cyanidin-3-Glucoside (C3G) retention.
Airborne Dispersion Elimination: Directly removes the physical catalysts of ambient airborne dispersion to safeguard cleanroom compliance on high-speed automated lines.
Operational Benefits for Dietary Supplement Manufacturers
Switching to Green Spring Technology’s engineered micro-granules yields measurable financial and operational advantages for manufacturing facilities. Traditional plant powders inherently slow down automated machinery, but optimizing physical morphology eliminates these systemic plant bottlenecks.
By addressing powder dynamics directly, brands realize higher throughput, minimal compliance risk, and superior final product uniformity.
Eradicating Airborne Cross-Contamination and Audit Risks
Ambient dust migration is a primary contributor to failed facility safety audits and cross-batch contamination fines. Green Spring Technology’s low-dust black rice extract remains contained within product hoppers, preventing loose particles from breaching HVAC containment zones. This strict particulate control simplifies compliance management under stringent third-party food safety frameworks like BRC and IFS.
Maximizing Powder Flowability to Prevent Machine Downtime
Poor powder flow leads to raw material bridging, rat-holing, and uneven die-filling during high-speed compression cycles. Our specialized fluid-bed granulation ensures a low Carr Index, allowing uniform flow through automated tablet presses and capsule-filling machines. This seamless flow eliminates mechanical jamming, decreases machine wear, and keeps high-throughput production lines running at peak capacity.
Accelerating Batch Changeovers and Cleaning Cycles
Heavy ambient dust coating machinery surfaces and cleanroom walls drastically extends required turnaround and washdown protocols. Because this engineered black rice extract generates minimal loose dust, facility crews complete physical tear-downs much faster. Shortening cleaning cycles translates directly to accelerated batch changeovers, maximizing Overall Equipment Effectiveness (OEE) and plant profitability.
Enhancing Dosage Uniformity and Material Yield
Uneven particle size distribution causes ingredients to segregate during blending, resulting in failed active ingredient uniformity assays. Our homogenous micro-granules lock in standardized Cyanidin-3-Glucoside (C3G) percentages, ensuring every single capsule contains identical potency. Additionally, eliminating fine dust prevents raw material loss via industrial vacuum dust-extraction systems, maximizing your final manufacturing yields.
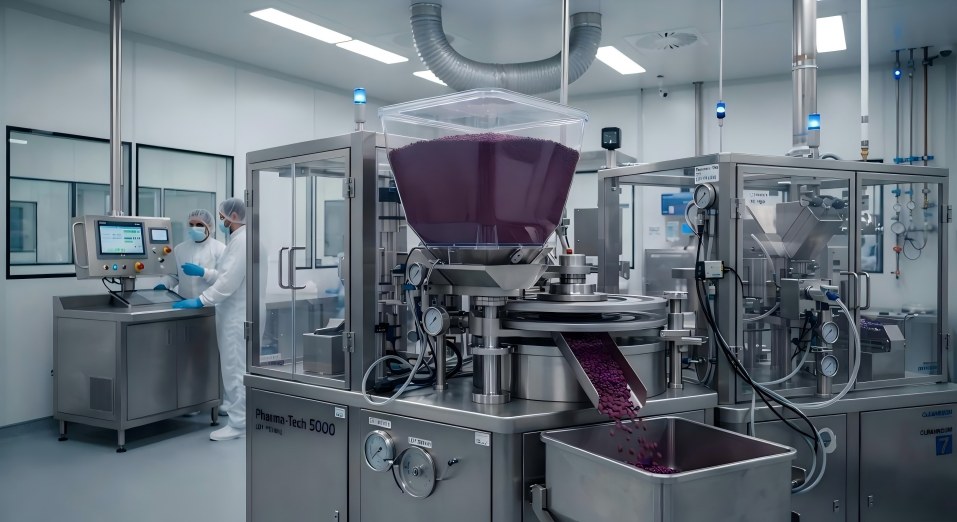
Physical Technical Parameters & Experimental Data Support
B2B qualification processes and R&D formulation frameworks rely heavily on rigorous, empirical evidence of raw material processability. Green Spring Technology provides verifiable physical parameters that demonstrate how structural particle manipulation directly optimizes manufacturing outcomes without altering chemical purity.
The data matrix below compares the functional processing metrics of conventional botanical powder fractions against our engineered micro-granules:
Physical Metric | Standard Black Rice Extract Powder | Green Spring Technology Low-Dust Micro-Granules |
Mesh Size & Structure | > 80–120 mesh fine powder | 40–80 engineered mesh (Spheroidal Micro-Granules) |
Dust Emission Tendency | High risk (airborne suspension) | Extremely low (< 3% airborne dispersion / Dust-free handling) |
Flow Properties (Carr Index) | Cohesive, poor flowability (Carr Index: 28–35) | Excellent free-flowing matrix (Carr Index: 11–15) |
Active Compound Content | Standardized C3G | Standardized C3G (Zero loss) |
Quantifiable improvements in bulk density and particle geometry significantly reduce material resistance inside automated feeding hoppers during high-speed compression cycles. Eliminating fine particulate fractions directly addresses the manufacturing trade-off between strict cleanroom contamination controls and target ingredient potency preservation.
This structural shift optimizes overall equipment effectiveness (OEE), allowing supplement brands to meet strict uniformity standards with absolute compliance confidence.
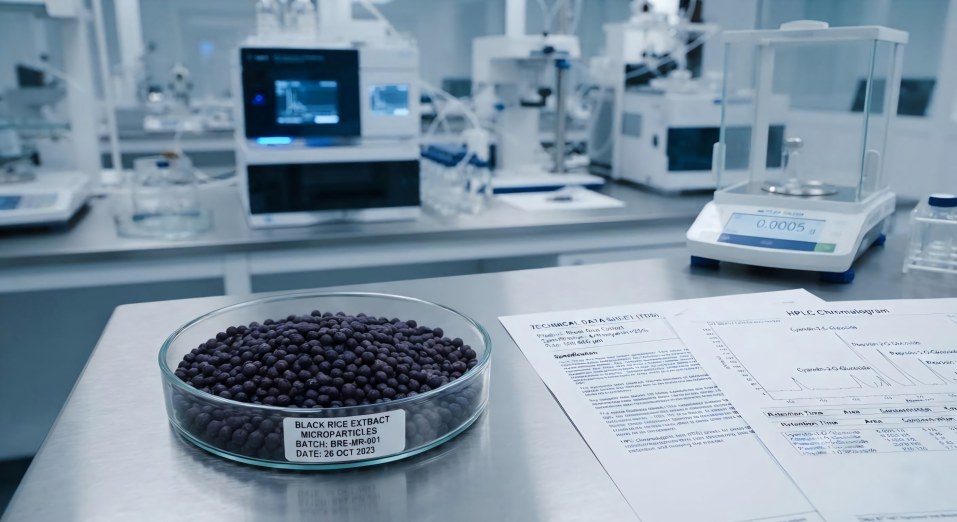
Premium Quality Compliance & Global Supply Chain Security
Green Spring Technology operates a fully audited, cGMP-compliant facility engineered to eliminate regulatory friction for international brands. Since 2000, our manufacturing protocols have enforced strict batch-to-batch consistency and comprehensive ingredient traceability.Every production run undergoes rigorous third-party verification to satisfy the most stringent multi-national quality control parameters.
Our low-dust black rice extract is fully backed by BRCGS, IFS, and active FDA registration to simplify supply chain risk management. Furthermore, our extraction processes adhere completely to Halal, Kosher, EU Organic, and USDA Organic standards for clean-label formulation compliance.
All batch-specific heavy metal profiles, pesticide screening data, and stability charts are available instantly to accelerate corporate procurement audits.
Step Into Your Next Production Run with Confidence
Test on Your High-Speed Lines: Get Your 50g Free Trial Sample to evaluate the actual free-flowing matrix and dust-free handling under real workshop conditions.
Verify Compliance Instantly: Request the Latest Batch COA & TDS to access complete HPLC fingerprint spectra, heavy metal analytics, and certified structural metrics.
-
Предыдущий
Phthalate-Free Black Rice Extract: Meeting Prop 65 and REACH Compliance
-
Следующий проект
Heat-Stable Black Rice Extract: Preserving Anthocyanins in Thermal Processing